
SEARCH WHAT YOU WANT
Workwear Fabrics: A Complete Guide from Protection Requirements to Application Matching
Time:2026-09-17
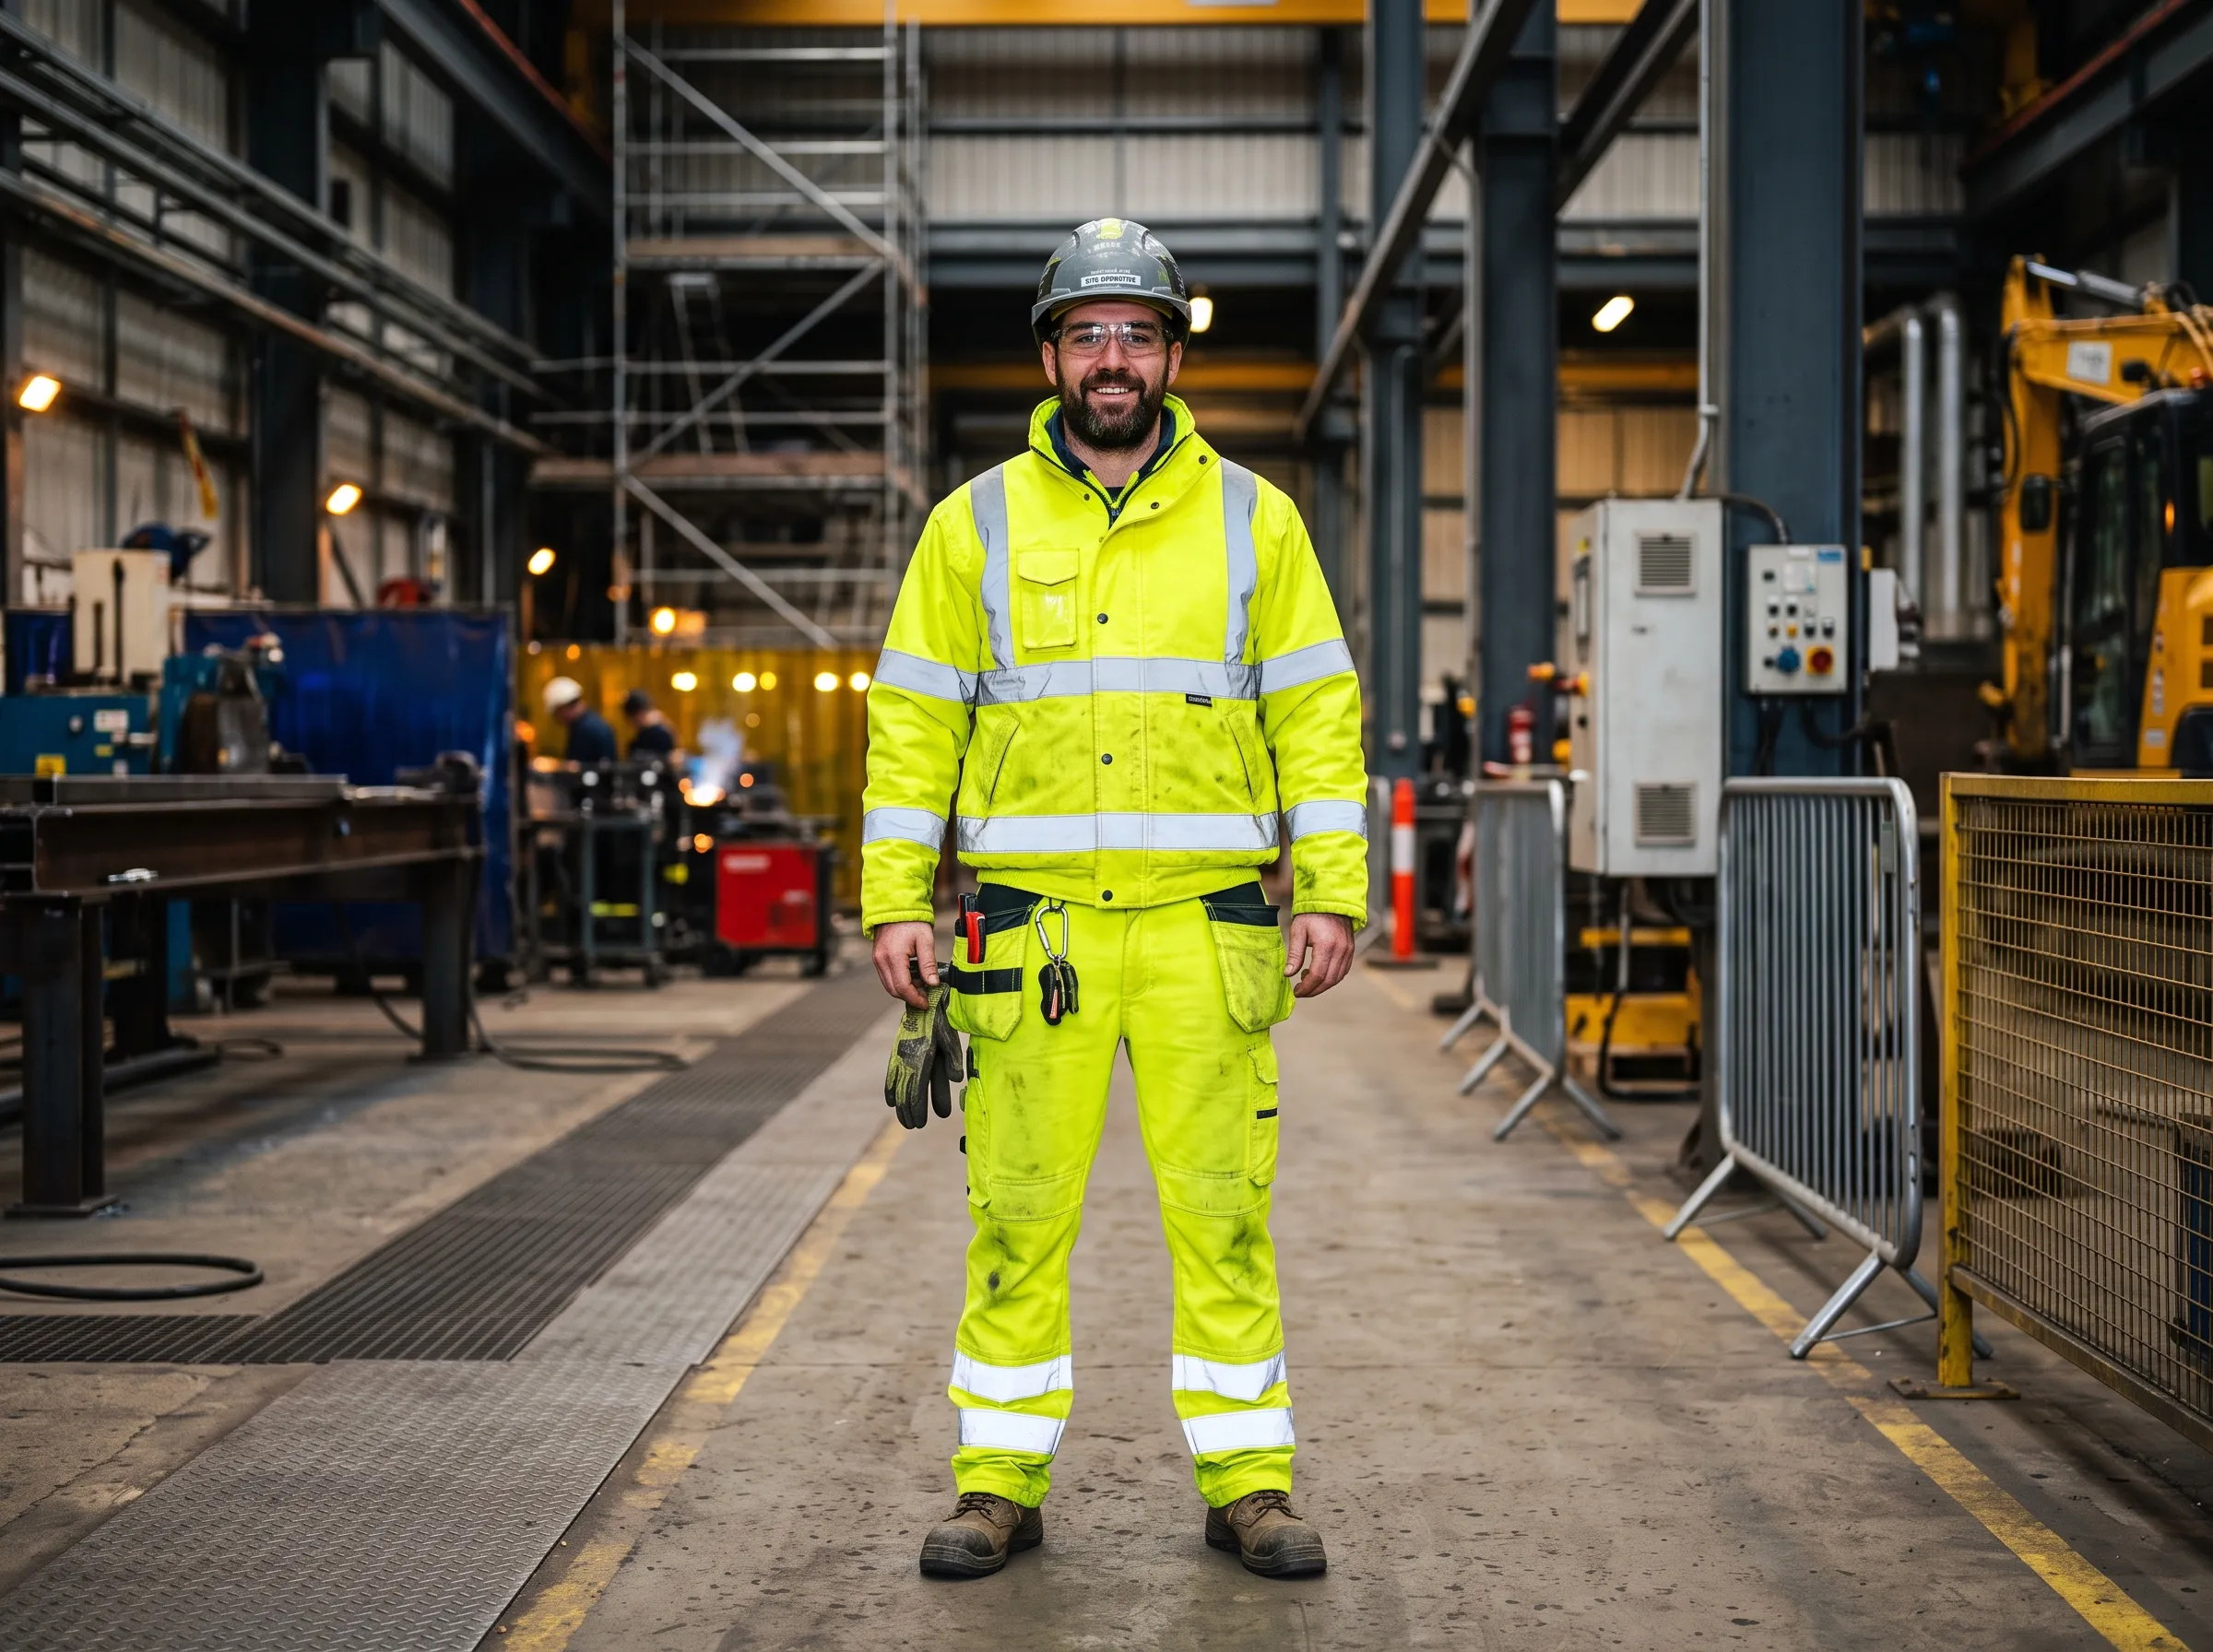
Workwear fabric is a specialized fabric designed for occupational apparel. It must precisely match diverse performance requirements—protection, comfort, durability, and easy-care—according to the specific operating conditions of different industries, while also accommodating the economic needs of bulk corporate procurement.
In sectors such as industry, services, and specialized operations, workwear fabric serves as the core foundational material for occupational protective equipment. This article systematically examines the selection logic and technological evolution of workwear fabrics across four dimensions: performance requirements, mainstream categories, application matching, and industry trends.
I. Core Performance: Four Dimensions That Define Workwear Fabric
The development of workwear fabrics revolves around four core dimensions: safety protection, long-term durability, wearing comfort, and cost-effectiveness.
1. Professional Protective Performance
Fabrics can be customized to deliver specific protective functions based on different working environments, effectively guarding against mechanical injury, chemical agent exposure, thermal radiation burns, and other occupational hazards. They also provide fundamental protective properties such as antibacterial and mildew resistance, acid and alkali resistance, and heat resistance.
Among these, flame-retardant workwear fabrics must strictly comply with authoritative domestic and international standards including GB 8965.1, EN 11612, and NFPA 2112. Anti-static workwear fabrics must meet the requirements of GB 12014 and EN 1149, suitable for safety requirements in flammable and explosive high-risk operating environments.
2. Long-Term Durability
Given the characteristics of high-frequency wear and frequent industrial laundering, workwear fabrics must deliver excellent tensile strength, tear resistance, abrasion resistance, and wrinkle resistance, with outstanding dimensional stability.
Conventional polyester-cotton blended fabrics achieve a shrinkage rate of only 1%-2% after five industrial wash cycles; pure cotton fabrics maintain shrinkage within 2%-3%; high-end functional flame-retardant fabrics can withstand 100 industrial wash cycles while maintaining stable protective performance and appearance quality, significantly extending the service life of workwear.
3. Wearing Comfort
Modern workwear fabrics have moved beyond the stereotype of being heavy and stiff. While ensuring protective performance, the focus has shifted to optimizing breathability, moisture management, and flexible resilience. Lightweight, high-elasticity fabrics have become the industry mainstream, adapting to body movement, reducing wearer fatigue, and accommodating special operating environments such as high temperature and high humidity.
4. Cost-Effectiveness
To meet the needs of bulk corporate procurement and unified distribution, workwear fabrics emphasize cost-effectiveness. Raw materials and production processes are mature and suitable for scaled manufacturing, effectively reducing corporate costs for workwear procurement, replacement, and maintenance, and accommodating routine workwear configuration needs across industries.
II. Mainstream Categories: Five Fabric Systems and Their Characteristics
Driven by textile technology iteration and increasingly refined industry demand, workwear fabrics have developed into a diversified product system with significant performance differentiation among categories.
1. Polyester-Cotton Blended Fabrics (T/C, CVC)
The most widely used general-purpose workwear fabric, combining the high-strength abrasion resistance, wrinkle resistance, and easy-care properties of polyester with the breathability and skin-friendly comfort of cotton.
Among these, CVC reverse-ratio polyester-cotton blended fabrics offer superior tensile strength, abrasion resistance, and wrinkle resistance compared to pure cotton, with stable dimensions and resistance to fading and pilling. They are suitable for the vast majority of conventional operating scenarios including workshops, offices, and general service industries.
2. Nylon/Polyamide Fabrics
Abrasion resistance ranks among the highest of natural and chemical fibers, combined with high strength, high toughness, and water- and wind-resistant properties. They resist stretching and deformation, and are primarily used in functional workwear for outdoor operations and engineering construction.
Nylon-cotton blended fabrics can undergo further deep functional finishing such as flame retardancy, three-proof finishing, and antibacterial treatment, suitable for high-end outdoor protection and other scenarios. Zhuofang possesses mature supply chain integration capabilities in high-tenacity nylon fabrics, providing workwear customers with integrated solutions from yarn selection to finished product delivery.
3. Functional Composite Coated Fabrics
Using polyester or nylon as the base fabric, these materials are combined with high-molecular functional materials such as polyurethane through coating, lamination, and layering processes, imparting special properties including weather resistance, flame retardancy, waterproof breathability, and anti-blocking performance.
These fabrics are subject to stringent process standards and are primarily used in high-demand scenarios such as outdoor protective equipment, high-end workwear, and specialized protective apparel. Zhuofang has mature quality control experience in coating and lamination processes for these fabrics. Through resident quality assurance teams, key indicators including coating thickness, uniformity, and peel strength are inspected batch by batch, ensuring stable and reliable functional performance in every meter of fabric.
4. High-End Flame-Retardant Fabrics
Divided into two major categories: inherently flame-retardant fiber fabrics and post-finishing flame-retardant fabrics.
Inherently flame-retardant fabrics represented by Nomex® have long served as benchmark protective materials in high-risk fields such as aviation, firefighting, and petrochemicals, owing to their stable heat resistance, flame retardancy, and anti-dripping performance. The new 88/12 cotton-nylon blended flame-retardant fabric balances the breathable comfort of cotton with the high strength and durability of nylon, offering greater cost-effectiveness and now widely used in various industrial flame-retardant workwear.
5. Specialized Fabrics
Several specialized fabrics have been developed for niche industry requirements:
-
Chef's check fabric: Moisture-absorbing, breathable, and pill-resistant, suitable for the food service industry
-
Specialized silk fabric: Anti-static and tear-resistant, suitable for the electronics and chemical industries
-
Fluorescent reflective Oxford fabric: Suitable for traffic, sanitation, and outdoor operations
-
Antibacterial, chlorine-bleach-resistant, low-elasticity slim-fit functional fabrics: Comprehensive coverage of niche application requirements
III. Application Matching: Selection Logic for Specific Industries
The selection of workwear fabrics follows the principle of "scenario matching and function alignment." Different industries select corresponding fabrics based on operating environment risks and work intensity.
| Industry Type | Recommended Fabric | Core Function |
|---|---|---|
| Heavy industries: construction, machinery, coal mining | Canvas, Oxford, high-density twill | High abrasion resistance, high strength, resistance to friction and impact |
| Flammable and explosive industries: electronics, petrochemicals, oil and gas, coal mines | Compliant anti-static fabrics | Eliminating static electricity hazards |
| High-risk industries: firefighting, chemicals, power | Compliant flame-retardant fabrics | Resistance to open flame and high-temperature thermal radiation |
| Medical and healthcare | Antibacterial, chlorine-bleach-resistant, easy-to-disinfect functional fabrics | Meeting hygiene protection standards |
| Food service | Chef's check fabric | Soft, breathable, easy to clean |
| Traffic, sanitation, municipal outdoor operations | Fluorescent reflective fabric | Enhancing outdoor visibility and safety |
| Office, security, and other routine scenarios | Skin-friendly, breathable, well-structured fabrics | Suitable for daily commuting and duty requirements |
IV. Trend Outlook: Four Iteration Directions
With the spread of green and low-carbon principles, the upgrading of intelligent manufacturing, and increasingly stringent industry safety standards, the workwear fabric industry is iterating toward four major directions: green sustainability, functional composite integration, intelligent lightweighting, and refined standardization.
1. Green Sustainability as the Core Theme
Environmentally friendly materials such as recycled polyester and bio-based fibers are being widely adopted. Recycled polyester workwear fabrics made from recycled PET bottles enable low-carbon circular production while offering excellent properties including antibacterial performance, anti-static function, and moisture-wicking quick-dry capability.
Fluorine-free water- and oil-repellent finishes and harmful-agent-free green finishing technologies are gradually replacing conventional processes, aligning with global textile green development standards and becoming new industry entry requirements.
2. Functional Composite Integration Replacing Single-Function Fabrics
Single-function fabrics—whether abrasion-resistant, anti-static, or flame-retardant alone—can no longer meet complex operating scenarios. Multi-functional composite fabrics such as flame-retardant + anti-static, waterproof + breathable + weather-resistant, and antibacterial + anti-static are rapidly gaining popularity, simultaneously addressing multiple operational risks in high-risk and complex industrial environments.
3. Continuous Upgrading of Product Experience and Production Technology
The industry is moving away from heavy, inefficient conventional fabrics, vigorously promoting lightweight, high-elasticity, environment-adaptive intelligent fabrics. Fabrics with new functions such as temperature-responsive regulation, self-repair, and environmental responsiveness are gradually being commercialized.
Meanwhile, digital and intelligent production, automated dyeing and finishing, and industrial standardized wash-compatibility technologies continue to mature, significantly improving fabric performance stability and production efficiency.
4. Continuous Optimization of Industry Standards and Market Landscape
Global workwear fabric testing and certification systems are becoming increasingly comprehensive, with industry protection standards continuously refined, driving product quality upgrades.
The Asia-Pacific region, leveraging its complete textile industry chain, mature production processes, and cost advantages, has become the global core production and export base for workwear fabrics. Domestic enterprises continue to strengthen their competitiveness in functional innovation, green production, and intelligent manufacturing.
V. Zhuofang's Workwear Fabric Solutions
Shanghai Zhuofang Textile Technology Co., Ltd., founded in 2014, is an innovative enterprise integrating R&D, production, and sales of functional textile fabrics and finished products. In the field of workwear fabrics, Zhuofang's business covers:
-
High-tenacity nylon and polyester fabrics
-
Waterproof breathable coated and laminated fabrics
-
Functional workwear protective fabrics
-
High-strength composite protective fabrics
-
Medical protective fabrics
-
Outdoor functional protective fabrics
Quality control is Zhuofang's core advantage. The company deeply integrates the high-quality supply chain of the Yangtze River Delta, stationing experienced quality assurance teams year-round at partner factories to conduct full-process quality inspection and process consistency verification across the three key stages of weaving, dyeing, and functional finishing. From raw material receiving to finished goods dispatch, every meter of fabric undergoes item-by-item verification.
The company operates a standardized testing laboratory equipped with precision testing instruments, strictly implementing international standards to conduct full-process quality control over key fabric metrics including strength, water resistance, dimensional stability, breathability, and color fastness. The company has obtained ISO9001 Quality Management System Certification and OEKO-TEX Environmental Certification, and supports SGS testing and certification.
With the mission of "safeguarding those who work in extreme environments," Zhuofang is committed to providing stable and reliable workwear fabric solutions for customers in labor protection, medical, outdoor, and other fields.
For workwear fabric selection advice or to request samples, please contact us.
Workwear fabric is a specialized fabric designed for occupational apparel. It must precisely match diverse performance requirements—protection, comfort, durability, and easy-care—according to the specific operating conditions of different industries, while also accommodating the economic needs of bulk corporate procurement.
In sectors such as industry, services, and specialized operations, workwear fabric serves as the core foundational material for occupational protective equipment. This article systematically examines the selection logic and technological evolution of workwear fabrics across four dimensions: performance requirements, mainstream categories, application matching, and industry trends.
I. Core Performance: Four Dimensions That Define Workwear Fabric
The development of workwear fabrics revolves around four core dimensions: safety protection, long-term durability, wearing comfort, and cost-effectiveness.
1. Professional Protective Performance
Fabrics can be customized to deliver specific protective functions based on different working environments, effectively guarding against mechanical injury, chemical agent exposure, thermal radiation burns, and other occupational hazards. They also provide fundamental protective properties such as antibacterial and mildew resistance, acid and alkali resistance, and heat resistance.
Among these, flame-retardant workwear fabrics must strictly comply with authoritative domestic and international standards including GB 8965.1, EN 11612, and NFPA 2112. Anti-static workwear fabrics must meet the requirements of GB 12014 and EN 1149, suitable for safety requirements in flammable and explosive high-risk operating environments.
2. Long-Term Durability
Given the characteristics of high-frequency wear and frequent industrial laundering, workwear fabrics must deliver excellent tensile strength, tear resistance, abrasion resistance, and wrinkle resistance, with outstanding dimensional stability.
Conventional polyester-cotton blended fabrics achieve a shrinkage rate of only 1%-2% after five industrial wash cycles; pure cotton fabrics maintain shrinkage within 2%-3%; high-end functional flame-retardant fabrics can withstand 100 industrial wash cycles while maintaining stable protective performance and appearance quality, significantly extending the service life of workwear.
3. Wearing Comfort
Modern workwear fabrics have moved beyond the stereotype of being heavy and stiff. While ensuring protective performance, the focus has shifted to optimizing breathability, moisture management, and flexible resilience. Lightweight, high-elasticity fabrics have become the industry mainstream, adapting to body movement, reducing wearer fatigue, and accommodating special operating environments such as high temperature and high humidity.
4. Cost-Effectiveness
To meet the needs of bulk corporate procurement and unified distribution, workwear fabrics emphasize cost-effectiveness. Raw materials and production processes are mature and suitable for scaled manufacturing, effectively reducing corporate costs for workwear procurement, replacement, and maintenance, and accommodating routine workwear configuration needs across industries.
II. Mainstream Categories: Five Fabric Systems and Their Characteristics
Driven by textile technology iteration and increasingly refined industry demand, workwear fabrics have developed into a diversified product system with significant performance differentiation among categories.
1. Polyester-Cotton Blended Fabrics (T/C, CVC)
The most widely used general-purpose workwear fabric, combining the high-strength abrasion resistance, wrinkle resistance, and easy-care properties of polyester with the breathability and skin-friendly comfort of cotton.
Among these, CVC reverse-ratio polyester-cotton blended fabrics offer superior tensile strength, abrasion resistance, and wrinkle resistance compared to pure cotton, with stable dimensions and resistance to fading and pilling. They are suitable for the vast majority of conventional operating scenarios including workshops, offices, and general service industries.
2. Nylon/Polyamide Fabrics
Abrasion resistance ranks among the highest of natural and chemical fibers, combined with high strength, high toughness, and water- and wind-resistant properties. They resist stretching and deformation, and are primarily used in functional workwear for outdoor operations and engineering construction.
Nylon-cotton blended fabrics can undergo further deep functional finishing such as flame retardancy, three-proof finishing, and antibacterial treatment, suitable for high-end outdoor protection and other scenarios. Zhuofang possesses mature supply chain integration capabilities in high-tenacity nylon fabrics, providing workwear customers with integrated solutions from yarn selection to finished product delivery.
3. Functional Composite Coated Fabrics
Using polyester or nylon as the base fabric, these materials are combined with high-molecular functional materials such as polyurethane through coating, lamination, and layering processes, imparting special properties including weather resistance, flame retardancy, waterproof breathability, and anti-blocking performance.
These fabrics are subject to stringent process standards and are primarily used in high-demand scenarios such as outdoor protective equipment, high-end workwear, and specialized protective apparel. Zhuofang has mature quality control experience in coating and lamination processes for these fabrics. Through resident quality assurance teams, key indicators including coating thickness, uniformity, and peel strength are inspected batch by batch, ensuring stable and reliable functional performance in every meter of fabric.
4. High-End Flame-Retardant Fabrics
Divided into two major categories: inherently flame-retardant fiber fabrics and post-finishing flame-retardant fabrics.
Inherently flame-retardant fabrics represented by Nomex® have long served as benchmark protective materials in high-risk fields such as aviation, firefighting, and petrochemicals, owing to their stable heat resistance, flame retardancy, and anti-dripping performance. The new 88/12 cotton-nylon blended flame-retardant fabric balances the breathable comfort of cotton with the high strength and durability of nylon, offering greater cost-effectiveness and now widely used in various industrial flame-retardant workwear.
5. Specialized Fabrics
Several specialized fabrics have been developed for niche industry requirements:
-
Chef's check fabric: Moisture-absorbing, breathable, and pill-resistant, suitable for the food service industry
-
Specialized silk fabric: Anti-static and tear-resistant, suitable for the electronics and chemical industries
-
Fluorescent reflective Oxford fabric: Suitable for traffic, sanitation, and outdoor operations
-
Antibacterial, chlorine-bleach-resistant, low-elasticity slim-fit functional fabrics: Comprehensive coverage of niche application requirements
III. Application Matching: Selection Logic for Specific Industries
The selection of workwear fabrics follows the principle of "scenario matching and function alignment." Different industries select corresponding fabrics based on operating environment risks and work intensity.
| Industry Type | Recommended Fabric | Core Function |
|---|---|---|
| Heavy industries: construction, machinery, coal mining | Canvas, Oxford, high-density twill | High abrasion resistance, high strength, resistance to friction and impact |
| Flammable and explosive industries: electronics, petrochemicals, oil and gas, coal mines | Compliant anti-static fabrics | Eliminating static electricity hazards |
| High-risk industries: firefighting, chemicals, power | Compliant flame-retardant fabrics | Resistance to open flame and high-temperature thermal radiation |
| Medical and healthcare | Antibacterial, chlorine-bleach-resistant, easy-to-disinfect functional fabrics | Meeting hygiene protection standards |
| Food service | Chef's check fabric | Soft, breathable, easy to clean |
| Traffic, sanitation, municipal outdoor operations | Fluorescent reflective fabric | Enhancing outdoor visibility and safety |
| Office, security, and other routine scenarios | Skin-friendly, breathable, well-structured fabrics | Suitable for daily commuting and duty requirements |
IV. Trend Outlook: Four Iteration Directions
With the spread of green and low-carbon principles, the upgrading of intelligent manufacturing, and increasingly stringent industry safety standards, the workwear fabric industry is iterating toward four major directions: green sustainability, functional composite integration, intelligent lightweighting, and refined standardization.
1. Green Sustainability as the Core Theme
Environmentally friendly materials such as recycled polyester and bio-based fibers are being widely adopted. Recycled polyester workwear fabrics made from recycled PET bottles enable low-carbon circular production while offering excellent properties including antibacterial performance, anti-static function, and moisture-wicking quick-dry capability.
Fluorine-free water- and oil-repellent finishes and harmful-agent-free green finishing technologies are gradually replacing conventional processes, aligning with global textile green development standards and becoming new industry entry requirements.
2. Functional Composite Integration Replacing Single-Function Fabrics
Single-function fabrics—whether abrasion-resistant, anti-static, or flame-retardant alone—can no longer meet complex operating scenarios. Multi-functional composite fabrics such as flame-retardant + anti-static, waterproof + breathable + weather-resistant, and antibacterial + anti-static are rapidly gaining popularity, simultaneously addressing multiple operational risks in high-risk and complex industrial environments.
3. Continuous Upgrading of Product Experience and Production Technology
The industry is moving away from heavy, inefficient conventional fabrics, vigorously promoting lightweight, high-elasticity, environment-adaptive intelligent fabrics. Fabrics with new functions such as temperature-responsive regulation, self-repair, and environmental responsiveness are gradually being commercialized.
Meanwhile, digital and intelligent production, automated dyeing and finishing, and industrial standardized wash-compatibility technologies continue to mature, significantly improving fabric performance stability and production efficiency.
4. Continuous Optimization of Industry Standards and Market Landscape
Global workwear fabric testing and certification systems are becoming increasingly comprehensive, with industry protection standards continuously refined, driving product quality upgrades.
The Asia-Pacific region, leveraging its complete textile industry chain, mature production processes, and cost advantages, has become the global core production and export base for workwear fabrics. Domestic enterprises continue to strengthen their competitiveness in functional innovation, green production, and intelligent manufacturing.
V. Zhuofang's Workwear Fabric Solutions
Shanghai Zhuofang Textile Technology Co., Ltd., founded in 2014, is an innovative enterprise integrating R&D, production, and sales of functional textile fabrics and finished products. In the field of workwear fabrics, Zhuofang's business covers:
-
High-tenacity nylon and polyester fabrics
-
Waterproof breathable coated and laminated fabrics
-
Functional workwear protective fabrics
-
High-strength composite protective fabrics
-
Medical protective fabrics
-
Outdoor functional protective fabrics
Quality control is Zhuofang's core advantage. The company deeply integrates the high-quality supply chain of the Yangtze River Delta, stationing experienced quality assurance teams year-round at partner factories to conduct full-process quality inspection and process consistency verification across the three key stages of weaving, dyeing, and functional finishing. From raw material receiving to finished goods dispatch, every meter of fabric undergoes item-by-item verification.
The company operates a standardized testing laboratory equipped with precision testing instruments, strictly implementing international standards to conduct full-process quality control over key fabric metrics including strength, water resistance, dimensional stability, breathability, and color fastness. The company has obtained ISO9001 Quality Management System Certification and OEKO-TEX Environmental Certification, and supports SGS testing and certification.
With the mission of "safeguarding those who work in extreme environments," Zhuofang is committed to providing stable and reliable workwear fabric solutions for customers in labor protection, medical, outdoor, and other fields.
For workwear fabric selection advice or to request samples, please contact us.
Previous: No more data

FABRIC FOR TECHNICAL PROTECTION
Copyright © 2025 Shanghai Brilliant Textile Co., Ltd.